Solid carbide drills and centre drilling
Seven series for specific jobs: general drilling, stainless and titanium, hardened steel, straight-flute drilling and sizing, flat bottoms, centre drilling. Depths from 3D to 50D without retracting the tool at every step.
We reply within the working day. There is no minimum order.
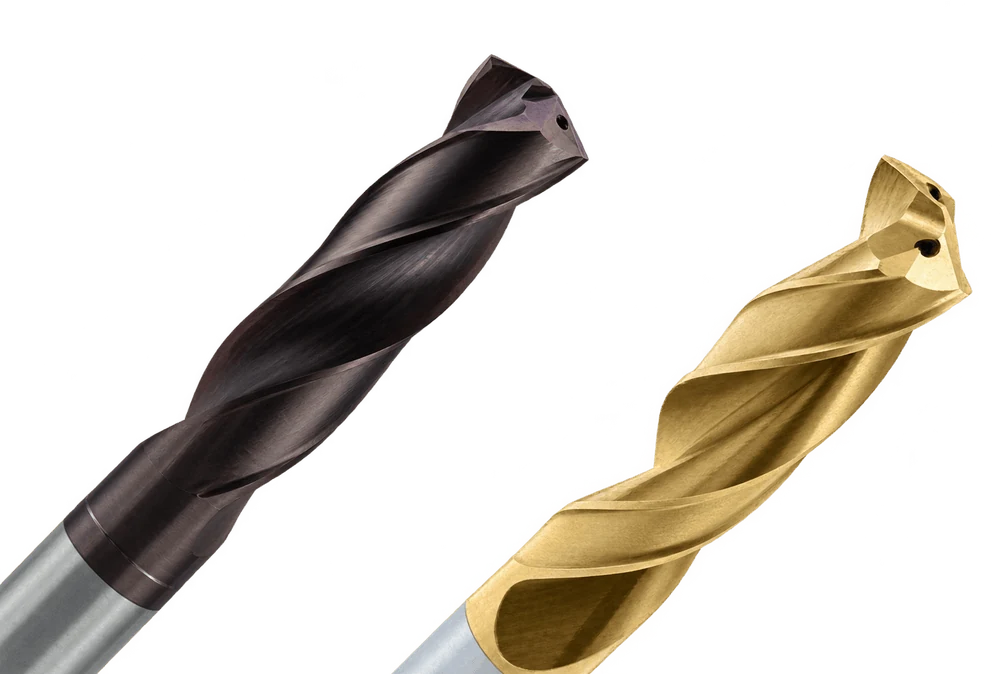
Model range
A drill works in a closed hole: there is nowhere for the chip to go, nowhere for the heat to go, and the point at the tip of the cutting cone has zero cutting speed. That is why there is no “universal” drill for all materials — each class has its own series with its own point angle, helix and coating.
The main series of the shop: structural and alloy steel, cast iron, stainless. A rigid body geometry holds the hole axis, and the self-centring 140° point enters the material without centre punching first.
DPC — internal coolant supply, from 3D to 30D. DPN — external, from 3D to 50D. In other words, one series covers both a through hole in a 10 mm plate and a deep cooling channel in a mould.
Materials that stretch rather than cut: austenitic stainless work-hardens right under the edge, and titanium and nickel alloys keep the heat in the cutting zone because they barely conduct it away.
The answer is a sharp geometry with a minimal edge radius and a nanolayer coating with a working temperature up to 1200 °C. The edge cuts instead of pushing; the chip does not weld itself to the flute.
Drilling into a heat-treated part — with no tempering, no EDM and no “we'll drill it before hardening”. A low helix angle makes the web thicker and the edge stronger in compression: that is exactly how the load is carried on hard material.
The typical job is holes for dowels and ejector pins in an already hardened mould, when the designer changed his mind after heat treatment.
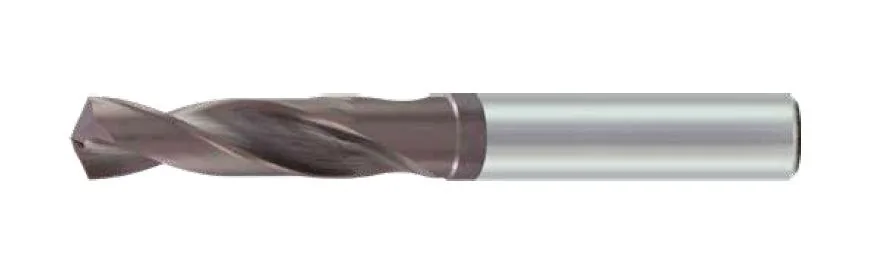
The working drill for the maintenance section and small batches: steel, stainless, cast iron, aluminium — with one tool, without choosing a series for every part. The 130° angle gives a gentler entry into the material on a less rigid machine.
This is deliberately the economical option. When a batch runs in one and the same material, a DP or a DM will give more.
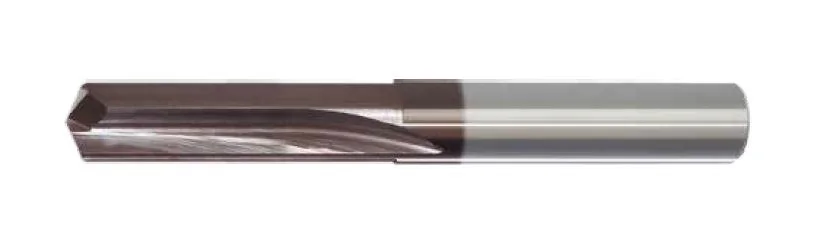
A straight flute instead of a helical one: the drill does not pull itself into the hole and does not tear the material out on exit. For cast iron, bronze, brass and plastics, where a twist drill leaves a broken edge on the exit side.
It drills and sizes in one pass — the hole comes out with a finish close to reaming, with no separate operation.
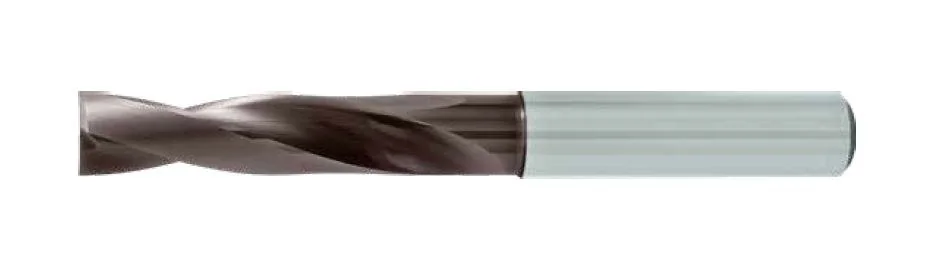
For jobs where an ordinary drill wanders off: entering an inclined or convex surface, drilling into an existing hole, a half hole at the joint of two parts, channels crossing at an angle.
A flat point has no place to slip from — the tool starts cutting with the whole edge at once. The bottom of the hole comes out flat, with no cone: for a face seat, for a seal, for the flat bottom of a pocket.
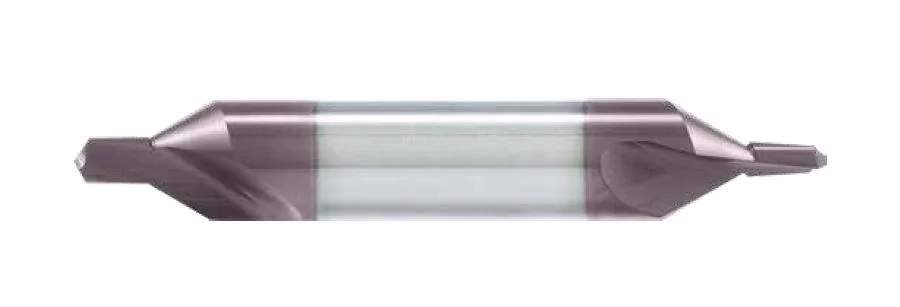
Carbide centre drilling instead of high-speed steel: a more rigid point does not wander over the surface and gives a spot from which the main drill will run true. On a CNC machine that is the difference between a hole within positional tolerance and a hole “somewhere near”.
Two countersink angles — 60° for centres used when working between centres, and 90° for a chamfer ready for a metric thread.
If you need a hole to an H7 fit, reaming follows the drilling. Carbide reamers with straight and helical flutes have a section of their own.
Coating
In drilling the coating matters more than in any other operation. The edge sits in a closed hole, the heat has nowhere to go, and the chip rubs along the flute over its whole length as it comes out. A bare carbide edge in stainless gives up in minutes.
That is why the KARASAWA programme does not have one “house” coating for the whole catalogue but a range: from economical multilayer TiAlN to nanolayer AlTiSiN with a working temperature of 1200 °C. The coating is selected together with the series — you get the right pairing rather than a set to choose from.
| Coating | Colour | Composition | Hardness HV0.05 | Working t° | Coeff. of friction | Structure | Where this works |
|---|---|---|---|---|---|---|---|
| ECObasic | TiAlN | 2800–3100 | 800–900 °C | 0,4–0,5 | multilayer | The DG and CC series. Everyday drilling of steel, cast iron and aluminium at moderate cutting data. When the job is ordinary and the tooling spend is being counted. | |
| ECO-Xsmooth | TiAlN | 2800–3100 | 800–900 °C | 0,3–0,4 | multilayer | The same chemistry, but with a polished surface: friction is roughly a quarter lower. In a deep hole that is decisive — the chip travels up the flute instead of packing into it. The DP, DK and DF series. | |
| MEGAnanolayer | AlTiSiN | 3500–3800 | 1100–1200 °C | 0,3–0,4 | nano, multilayer | The silicon in it raises the hardness of the layer by about a quarter and the working temperature ceiling by 300 °C. Stainless, titanium, nickel alloys, hardened steel: the DM and DH series. |
How to read this in practice. The difference between ECO and ECO-X is not in wear resistance but in how the chip comes away: the same geometry with a smooth coating lets you go deeper without retracting the tool. The difference between ECO-X and MEGA is the temperature ceiling: while the cutting zone stays below 900 °C both work; above that, only MEGA is left.
Selection
A table for solid carbide drills with a hole tolerance within 0…+0.1 mm. The first column is the main recommendation, the second a workable alternative if the first is out of stock or the machine is less rigid.
| Material group | Examples | First recommendation | Second recommendation | Comment |
|---|---|---|---|---|
| Psteel | S235, C45, 42CrMo4, cast steel | DP · ECO-X | DM · MEGA | The base case. The DM is taken when the steel is alloyed and there is too much heat in the cutting zone. |
| Mstainless | AISI 304, 316, 321, duplex | DM · MEGA | DP · ECO-X | Work hardening under the edge. Do not reduce the feed “to be on the safe side” — a low feed is exactly what kills a drill in stainless. |
| Kcast iron | Grey, ductile and malleable cast iron | DP · ECO-X | DM · MEGA | For through holes with a requirement on the exit edge — the straight-flute DK. |
| Naluminium, brass | 2024 aluminium, AlSi, bronze, brass, copper | DG · ECO | — | The main problem is not wear but adhesion. Keep the feed high and do not let the chip stay in the flute. |
| Sheat-resistant, titanium | Inconel, Ti-6Al-4V, Hastelloy | DM · MEGA | DH · MEGA | Reducing the cutting speed works here; reducing the feed does not. Internal coolant is desirable from 3D onwards. |
| Hhardened steel | Tool steel after heat treatment | DH · MEGA | — | Rigid clamping and a minimal overhang. Runout above 0.02 mm decides the fate of the drill faster than the cutting data does. |
Within a series you then choose the version: internal or external coolant supply, and the depth in diameters — 3D, 5D, 7D and beyond.
In summary
A hole is rarely an end in itself — it is drilled so that a thread can be cut, a dowel fitted or oil passed through. The cost of a mistake at this operation is always higher than the cost of the drill itself: the part has already been through the earlier operations.
Centre drilling, drilling, reaming and flat bottoms are covered by one programme. One price list, one delivery note, one person to agree lead times with.
You do not have to decide which coating to specify for stainless and which for cast iron. The series arrives with the right coating — the decision was made at the catalogue stage.
Common diameters are held in stock. The most expensive drill is not the one that costs a lot but the one that is not there on the day a part stops in production.
